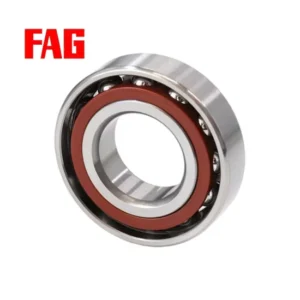
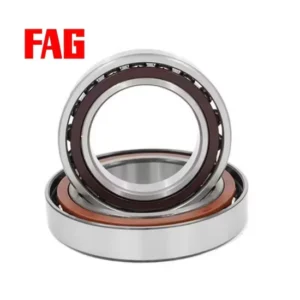
Product Details
About This INA Bearing
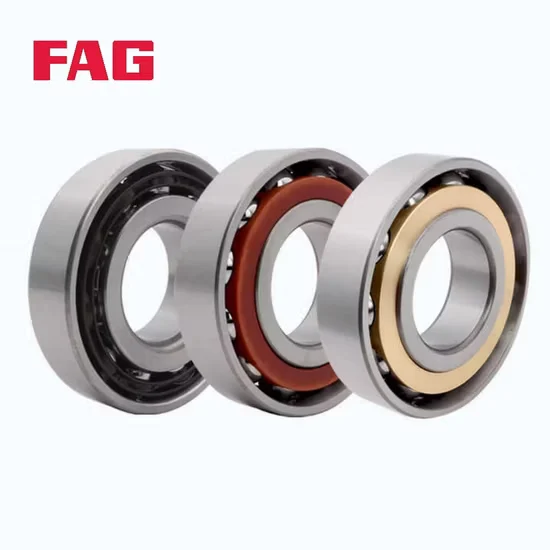
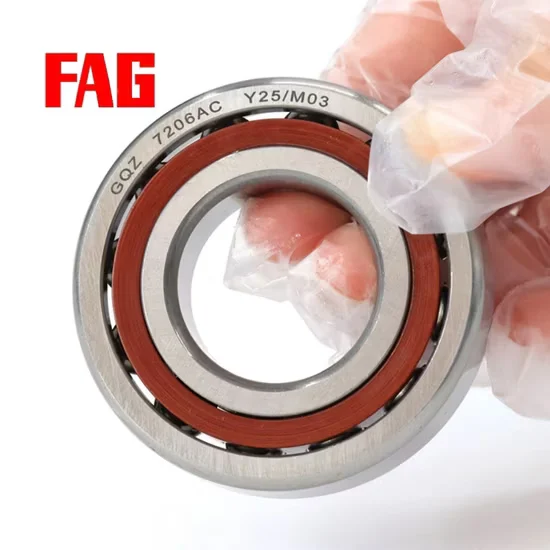
Original Batch Traceability — Every FAG HS7026-C-T-P4s-UL angular contact ball bearing ships with verifiable factory lot documentation to ensure authentic spindle performance.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | FAG HS7026-C-T-P4s-UL |
| Bearing Type | Angular Contact Ball Bearing |
| Precision Class | P4s |
| Contact Angle | 15° |
| Material | Steel |
| Origin | Jiangsu China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Machine Tool Manufacturing | High-speed machining center spindles |
| Precision Engineering | CNC lathe main shafts |
| Industrial Automation | High-speed pump drives |
Why Spindle Vibration Ruins Tolerances Before the FAG HS7026-C-T-P4s-UL Angular Contact Ball Bearing Fails
Improper preload matching causes thermal expansion that destroys machining accuracy long before physical bearing fatigue occurs.
When replacing spindle bearings on a five-axis machining center in Suzhou, mismatching the universal preload pairing led to severe thermal growth during high-speed cutting. The resulting vibration scrapped a batch of precision aerospace components. Sourcing the correct FAG HS7026-C-T-P4s-UL angular contact ball bearing requires strict adherence to pairing marks to prevent catastrophic thermal runaway. Many maintenance teams assume that simply pressing a high-precision component into the housing guarantees performance, ignoring the microscopic variations in internal clearance. This oversight generates excessive friction at elevated RPMs, causing the spindle nose to expand unpredictably and ruin tight geometric tolerances.
Matching Preload Stiffness to High-Speed Cutting Forces
High-speed milling demands a precise balance between radial rigidity and axial displacement control. The FAG HS7026-C-T-P4s-UL angular contact ball bearing delivers the necessary axial stiffness through its optimized contact geometry, ensuring the spindle nose maintains strict dimensional accuracy under varying cutting loads. Our technical team cross-checks your specific machining parameters to confirm this configuration aligns with your operational demands. If the internal preload is too light, the tool will chatter during heavy roughing passes, leaving poor surface finishes. Conversely, excessive preload generates unnecessary heat, accelerating lubricant degradation and shortening the operational lifespan of the assembly.
Managing Thermal Growth and Lubrication Starvation
Spindle environments subject bearings to extreme rotational speeds where friction-induced heat rapidly degrades lubricant films. At elevated temperatures, the internal clearance diminishes, increasing the risk of seizure if the initial preload is not carefully calculated. Proper oil-air or grease lubrication intervals must be established to manage heat dissipation while preventing contamination ingress. The 15° contact angle helps distribute these dynamic loads effectively across the raceway, minimizing localized stress concentrations. Furthermore, the sealing arrangement must be evaluated to ensure it keeps microscopic coolant mist and metallic swarf out of the raceway without introducing excessive drag that would compound the thermal challenges.
Decoding the P4s Precision and 15° Contact Geometry
The P4s precision class dictates exceptionally tight dimensional and running tolerances, which are mandatory for minimizing non-repetitive runout in precision grinding and milling operations. A 15° contact angle provides an optimal compromise, offering sufficient axial load capacity to handle thrust forces from tool engagement while maintaining the low friction characteristics required for high RPM limits. The steel construction ensures reliable structural integrity under continuous cyclic loading, though ceramic hybrid variants are available in the broader series for extreme speed applications. Achieving this level of precision requires advanced manufacturing techniques that control the raceway curvature and surface finish to an exacting standard, ensuring smooth rolling element transition and minimal vibration signature during operation.
The Financial Impact of Spindle Downtime and Scrap
Selecting an incorrect precision class or ignoring preload specifications leads to unplanned downtime and catastrophic damage to the spindle housing. According to ISO 15243 frameworks, improper mounting and preload errors are primary drivers of premature spindle failure, resulting in scrapped workpieces and expensive shaft repairs. The cost of a single scrapped titanium aerospace part vastly exceeds the investment in verified, correctly paired spindle components. When a spindle seizes unexpectedly, the collateral damage often extends to the motor couplings and labyrinth seals, turning a standard maintenance procedure into a major machine tool rebuild. Avoiding these hidden costs requires a disciplined approach to component verification and installation protocols.
Securing Authentic Spindle Components Through Rigorous Verification
Counterfeit or mislabeled precision bearings introduce unpredictable runout that ruins surface finishes. We supply the genuine FAG HS7026-C-T-P4s-UL angular contact ball bearing with complete batch traceability, ensuring the P4s tolerances are authentic. Our engineers verify the exact contact angle and preload suffixes against your machine tool requirements, preventing the costly mismatch errors I witnessed early in my career. We consolidate mixed-brand spindle packages, providing reliable global shipping without the extended lead times of direct factory channels. Every shipment is backed by comprehensive documentation that proves the origin and specification compliance of the components, giving maintenance managers the confidence needed to authorize critical machine restarts.
Documentation & Authenticity
- Certificate of Conformity validating the P4s precision grade for this specific batch.
- Original factory lot traceability documents linking the bearing to its production date.
- Dimensional and running accuracy inspection reports confirming tight spindle tolerances.
- Official manufacturer QR verification codes for immediate anti-counterfeiting validation.
Storage, Handling & Mounting
- Keep the matched set sealed in its original packaging until mounting to preserve the factory-applied rust preventive coating.
- Verify the universal pairing marks on the outer rings before installation to ensure correct preload alignment.
- Use clean, lint-free gloves when handling the P4s precision raceways to prevent microscopic corrosion from skin moisture.
- Employ controlled induction heating for the inner ring mounting, strictly monitoring the temperature to avoid altering the steel microstructure.
Providing Technical Parameters for Selection Review
To ensure the selected configuration matches your spindle design, please provide the exact radial and axial cutting loads, maximum operating RPM, and target spindle nose displacement limits. Sharing the original equipment manufacturer part number allows our engineering team to perform a precise cross-reference check. This data enables us to validate the L10 life calculation and confirm the optimal lubrication strategy for your specific machining environment. We also review the housing and shaft tolerance grades to ensure the interference fits will not inadvertently squeeze the bearing rings and alter the factory-set internal clearance during the mounting process.
Frequently Asked Questions
Q: How can I verify the authenticity of the P4s precision grade?
A: Authenticity is confirmed through the manufacturer's official verification app using the QR code on the packaging, alongside a physical Certificate of Conformity. We also provide original batch traceability documentation that links the specific FAG HS7026-C-T-P4s-UL angular contact ball bearing to its factory production run, ensuring the tight dimensional tolerances meet genuine specifications.
Q: What do the T and UL suffixes indicate in this part number?
A: Certain suffixes in complex spindle bearing designations remain unverified without direct manufacturer catalog confirmation to define exact cage materials or specific preload values. We always cross-reference these unverified suffixes with the official engineering documentation before shipment to guarantee the bearing matches your machine tool's precise axial stiffness and speed requirements.
Q: How should I interpret the 15° contact angle for my spindle?
A: A 15° contact angle optimizes the balance between high-speed capability and axial load capacity, making it ideal for high-RPM milling and grinding spindles. It provides lower friction compared to steeper angles, reducing heat generation during continuous operation while still maintaining sufficient rigidity to handle the thrust forces generated during tool engagement.
Q: What installation practices prevent preload mismatch errors?
A: Always keep the matched set sealed until the exact moment of mounting and strictly follow the factory alignment marks etched on the outer rings. Misaligning these marks during assembly alters the internal clearance, leading to severe thermal growth and vibration at high speeds, which is a common cause of premature spindle failure.