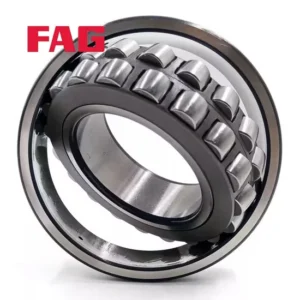
Product Details
About This INA Bearing
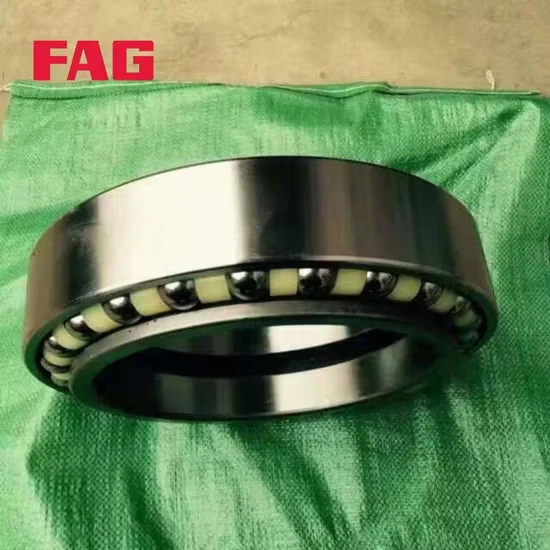
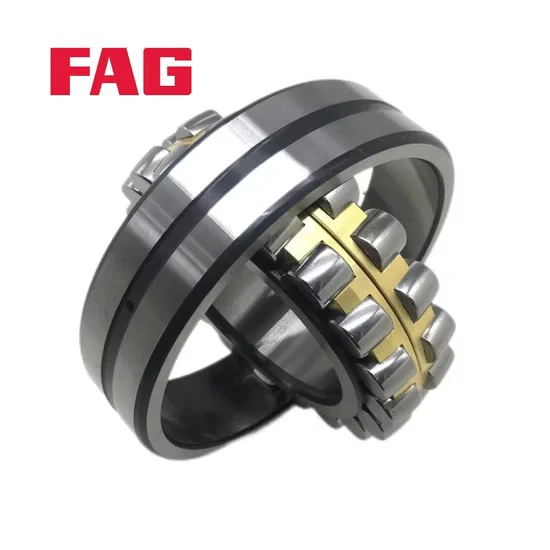
Original Batch Traceability — Every FAG 22220-E1-XL-K spherical roller bearing ships with factory batch records linking directly to the Schaeffler production facility.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | FAG 22220-E1-XL-K |
| Bearing Type | Spherical Roller Bearing |
| Bore Type | 1:12 Tapered Bore |
| Internal Design | Enhanced Capacity |
| Structure | Double Row, Self-Aligning |
| Material | Chrome Steel Gcr15 |
| Origin | Jiangsu China |
Note: E1 and XL suffixes denote specific internal design and X-life performance enhancements; verify exact manufacturer catalog definitions for this batch.
Application Suitability
| Industry | Typical Applications |
|---|---|
| Mining & Quarrying | Vibrating screen shaft mechanisms |
| Metallurgy | Continuous caster roll guides |
| Heavy Construction | Crusher eccentric shaft assemblies |
Why Premature Spalling Destroys the FAG 22220-E1-XL-K spherical roller bearing Before Fatigue Limits
Improper mounting heat destroys the microstructure long before dynamic loads cause fatigue.
During my early years in heat treatment and grinding at a Suzhou workshop, I watched a steel mill client use an open torch to heat a spherical roller bearing for a rolling mill. The uncontrolled flame destroyed the metallographic structure, triggering premature spalling. This harsh reality dictates my current technical sales approach: insisting on controlled induction heating and specifying XL series designs for heavy-duty applications where thermal stability and vibration resistance are critical. When procurement engineers overlook these fundamental mounting practices, the resulting microstructural damage compromises the entire assembly long before dynamic loads cause natural fatigue.
Procurement engineers often focus solely on dimensional equivalency while neglecting the metallurgical integrity required for high-stress environments. A component that matches the outer diameter and width specifications will still fail prematurely if the internal geometry cannot handle the specific shock loads of a vibrating screen. This is where deep technical validation becomes essential, bridging the gap between basic catalog data and actual field performance.
Aligning the FAG 22220-E1-XL-K spherical roller bearing With Heavy Shock Loads
Industrial facilities operating vibrating screens and continuous casters require components that can withstand severe radial forces and constant misalignment. The self-aligning capability of this design compensates for shaft deflections, ensuring smooth operation even under extreme mechanical stress. Our engineering team provides comprehensive cross-reference consultation to verify that this specific configuration matches your original equipment requirements, eliminating the guesswork from complex replacement projects and ensuring optimal performance.
Managing Thermal Expansion and Misalignment in Steel Mill Equipment
Heavy shock loads from crushers and vibrating screens demand a double row, self-aligning structure to accommodate continuous shaft deflections without binding. Temperature gradients in metallurgy applications significantly affect internal clearance, making proper lubrication intervals critical to prevent contamination ingress and friction heat buildup. Ignoring these thermal dynamics often results in uneven load distribution across the rolling elements.
Decoding the Tapered Bore and Enhanced Internal Geometry
The 1:12 tapered bore allows for precise interference fits when mounted on adapter sleeves, providing exceptional gripping force on the shaft. This specific internal geometry optimizes the roller profile and raceway contact area, distributing radial loads more evenly across the double row to increase the dynamic load rating. The XL series designation indicates a performance-enhanced design that extends the operational service life in heavy-duty environments. Proper installation requires measuring the drive-up distance to maintain the correct residual clearance, preventing excessive preload that could generate destructive friction heat.
Furthermore, the material composition and heat treatment processes play a vital role in determining the fatigue limit of the rings and rolling elements. Components manufactured from high-quality chrome steel undergo rigorous quality assurance protocols to ensure consistent hardness and dimensional stability. This metallurgical consistency is what allows the enhanced internal design to deliver its full load-carrying potential without suffering from early surface distress.
The Hidden Downtime Costs of Ignoring Suffix Configurations
Selecting an incorrect bore type or ignoring the enhanced internal geometry leads to unplanned downtime and catastrophic equipment damage in critical machinery. Misaligned shafts combined with improper clearance selections accelerate premature fatigue, ultimately voiding manufacturer warranties and inflating maintenance budgets. Following standardized failure analysis frameworks helps procurement teams identify these root causes before they escalate into complete system breakdowns.
The financial impact of these failures extends far beyond the replacement cost of the component itself. Unplanned shutdowns in a steel mill or mining operation halt entire production lines, resulting in substantial revenue losses and delayed project timelines. By prioritizing precise suffix configuration and verified sourcing channels, maintenance teams can significantly reduce the frequency of these disruptive events and improve overall equipment effectiveness.
Securing Authentic XL Series Bearings Through Verified Channels
Sourcing genuine components requires strict verification, as confusing standard internal designs with the specific enhanced geometry is a common procurement error that compromises performance. We provide complete factory batch traceability and cross-reference validation to ensure exact dimensional equivalency for every shipment. Our massive spot inventory covers thousands of standard part numbers, enabling flexible mixed-brand consolidation shipments without compromising authenticity or long-term technical support for failure analysis. This comprehensive approach ensures that every replacement part integrates flawlessly into your existing machinery, maximizing uptime and operational reliability.
Documentation & Authenticity
- Certificate of Conformity matching the specific FAG 22220-E1-XL-K batch number.
- Original factory traceability documents linking to the Schaeffler production facility.
- Official app QR code verification for anti-counterfeiting validation.
- Dimensional inspection reports confirming the 1:12 tapered bore tolerance.
Storage, Handling & Mounting
- Store in original packaging to protect the tapered bore from humidity and corrosion.
- Use controlled induction heating for mounting; open flames will destroy the metallographic structure.
- Verify the drive-up distance and residual clearance when mounting on adapter sleeves.
- Apply clean gloves when handling to prevent surface contamination before installation.
Preparing Your Technical Parameters for Cross-Reference Validation
To ensure precise selection and L10 life verification, please share your specific operating parameters including radial and axial loads, rotational speed, and ambient temperature. Providing the original equipment manufacturer part numbers allows our engineering team to perform accurate cross-reference validation and confirm dimensional equivalency for your machinery.
Frequently Asked Questions
Q: How to verify the authenticity of FAG bearings through official traceability channels?
A: Buyers can scan the official QR code using the manufacturer's mobile application to confirm the anti-counterfeiting status. Additionally, cross-check the original factory batch traceability documentation and certificates to ensure the FAG 22220-E1-XL-K spherical roller bearing matches the specific production records from the Schaeffler facility.
Q: What are the cross-reference precautions regarding clearance and precision alignment?
A: When cross-referencing to equivalent models from other brands, buyers must verify that the internal geometry and clearance class match the original equipment requirements. Mismatched clearance or precision alignment can lead to premature fatigue, so always consult technical documentation to confirm exact dimensional and operational equivalency.
Q: How does the enhanced internal design improve load capacity compared to standard designs?
A: The enhanced internal geometry optimizes the roller profile and raceway contact area, distributing radial loads more evenly across the double row. This structural improvement significantly increases the dynamic load rating and extends the operational service life in heavy-duty applications like vibrating screens and crushers.
Q: What are the mounting procedures for bearings with a 1:12 tapered bore?
A: Mounting requires an adapter sleeve to achieve the correct interference fit on the shaft. Technicians must measure the drive-up distance and check the residual clearance to prevent excessive preload. Controlled induction heating is mandatory, as localized flame heating destroys the steel's microstructure and causes early spalling.