



Product Details
About This INA Bearing
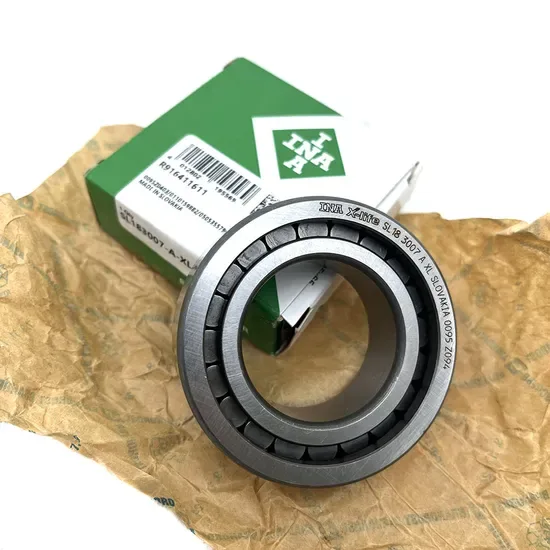
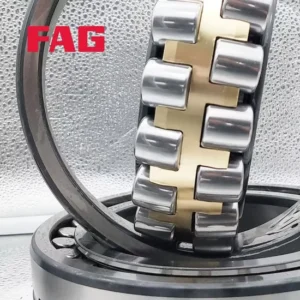
Factory QR Verification — Scan the manufacturer's app code on the packaging to confirm the exact production batch of this FAG 22308-E1-XL-K-C3 spherical roller bearing before installation.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | FAG 22308-E1-XL-K-C3 |
| Bearing Type | Spherical Roller Bearing |
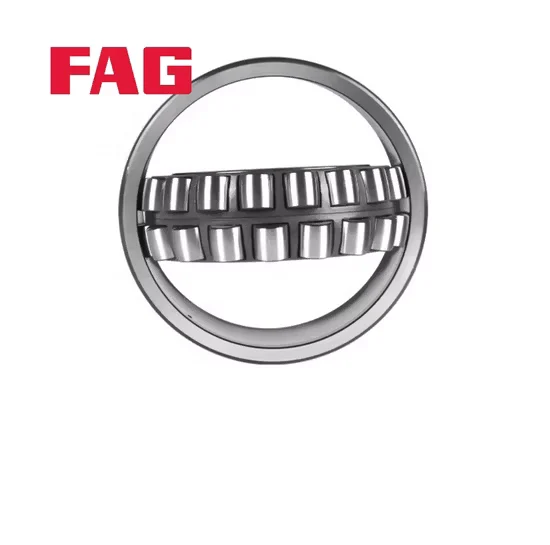
| Structure | Double Row, Self-Aligning |
| Bore Type | Tapered Bore (1:12 Taper) |
| Clearance Class | C3 |
| Main Material | Chrome Steel |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Mining & Construction | Vibrating screen eccentric shafts, crusher main frames |
| Steel & Metallurgy | Continuous caster roll segments, rolling mill gearboxes |
| Pulp & Paper | Paper machine dryer cylinder journals |
Why Tapered Bore Spherical Roller Bearings Fail During Heat Mounting
Direct flame heating destroys the metallurgical structure, leading to rapid thermal seizure under heavy loads.
During my time handling aftermarket support for mining sites in Nigeria, I watched maintenance crews apply open torches directly to the inner rings of spherical roller bearings. This reckless practice alters the heat treatment, dropping the hardness well below specification and causing catastrophic shaft lock-ups within weeks. Proper induction heating is non-negotiable for preserving the integrity of the FAG 22308-E1-XL-K-C3 spherical roller bearing when mounting on adapter sleeves.
Matching the Tapered Mount to Heavy-Duty Shafts
Securing a tight fit on a tapered shaft requires precise driving distances to maintain the correct residual internal clearance. Our engineering team provides cross-brand equivalent model consultation to ensure the adapter sleeve dimensions perfectly match the 1:12 taper profile. This prevents micro-movements that typically fret the shaft surface during high-vibration operations.
Navigating Thermal Expansion and Misalignment in Crushers
Vibrating screens and crushers subject equipment to severe shock loads and continuous shaft deflection. The double row self-aligning structure compensates for these angular misalignments, preventing edge loading on the rollers. Furthermore, elevated operating temperatures demand adequate internal clearance to accommodate thermal expansion of the shaft and housing. Selecting the correct lubrication interval is equally critical to flush out abrasive mining dust.
Decoding the Internal Clearance and Bore Geometry
The K suffix indicates a 1:12 tapered bore, designed specifically for mounting on adapter sleeves or tapered shafts to achieve a secure interference fit. The C3 clearance class provides extra internal space, which is essential when the inner ring expands due to friction heat or when the shaft operates at higher temperatures than the housing. This extra clearance prevents the rollers from skidding and binding under thermal growth. The double row configuration distributes heavy radial loads evenly across both rows of symmetrical spherical rollers.
The Hidden Costs of Improper Adapter Sleeve Tightening
Failing to tighten the adapter sleeve lock nut to the specified driving distance results in a loose inner ring fit. This looseness leads to micro-slip between the shaft and the bore, generating severe fretting corrosion that compromises the entire assembly. According to failure analysis frameworks, such mounting errors account for a significant share of premature failures in heavy machinery. The resulting unplanned downtime far exceeds the initial cost of precision tooling.
Securing Traceability for Critical MRO Replacements
Sourcing genuine components is critical when replacing heavily loaded spherical roller bearings. We provide complete traceability documentation for every FAG 22308-E1-XL-K-C3 spherical roller bearing, ensuring you receive original products with verified metallurgical properties. Our flexible MOQ supports both single-unit emergency spare-part orders for immediate breakdown recovery and full container consolidation for scheduled plant overhauls. We also offer cross-reference validation to confirm dimensional interchangeability if you are upgrading from legacy equipment setups.
Documentation & Authenticity
- Certificate of Conformity confirming the original manufacturer's production facilities and batch codes.
- Official app QR verification linking the physical box to the digital traceability ledger.
- Dimensional inspection report validating the 1:12 tapered bore geometry before dispatch.
- Material test certificate verifying the chrome steel composition and heat treatment compliance.
Storage, Handling & Mounting
- Keep the bearing in its original vapor-phase inhibitor packaging until the exact moment of mounting to prevent humidity corrosion on the precision-ground tapered bore.
- Use calibrated induction heaters with automatic demagnetization to expand the inner ring without altering the chrome steel microstructure.
- Measure the driving distance of the adapter sleeve lock nut meticulously to preserve the designated C3 internal clearance after mounting.
- Apply clean lint-free gloves when handling the exposed roller profiles to avoid acidic skin residue causing localized surface degradation.
Engineering Review for Your Next Procurement
Share your specific operating parameters, including radial and axial load profiles, operating temperatures, and shaft deflection limits, so our technical team can verify the L10 life calculation. Providing the OEM equipment model number allows us to perform a precise cross-reference check against your existing setup. This ensures the selected configuration perfectly matches your maintenance intervals and environmental conditions.
Frequently Asked Questions
Q: How can I verify the authenticity and original batch of this bearing?
A: You can authenticate the bearing by scanning the QR code on the packaging using the manufacturer's official mobile application. This digital verification links the physical product to its original production batch, confirming the metallurgical specifications and manufacturing origin. We also supply a Certificate of Conformity with every shipment to guarantee complete traceability for your records.
Q: What are the specific mounting requirements for the 1:12 tapered bore?
A: Mounting a 1:12 tapered bore requires an adapter sleeve and a lock nut tightened to a precise driving distance. This distance must be measured accurately using a feeler gauge to check residual internal clearance, ensuring the inner ring expands enough for a secure shaft grip without eliminating the designated C3 clearance necessary for thermal expansion.
Q: When is it necessary to select C3 clearance over standard internal clearance?
A: C3 clearance is required when the inner ring operates at a noticeably higher temperature than the outer ring, causing differential thermal expansion. It is also specified for applications involving heavy interference fits on tapered shafts, where the mounting process inherently reduces the internal clearance. This extra space prevents the rollers from binding under operational heat.
Q: How should I interpret the E1 and XL suffixes in this designation?
A: While the K and C3 suffixes definitively indicate a 1:12 tapered bore and increased internal clearance respectively, the E1 and XL designations are currently unverified suffixes requiring manufacturer catalog confirmation. We recommend consulting the official technical documentation or requesting our engineering team to cross-check these specific identifiers against the latest production standards.